Horizontal radial-axial ring rolling machines for large forged rings.
CNC Ring Rolling Machine
Wiz Forging Machinery manufactures CNC horizontal ring rolling machines for seamless forged rings. Machine configuration is engineered around your ring drawings, material and production requirements.
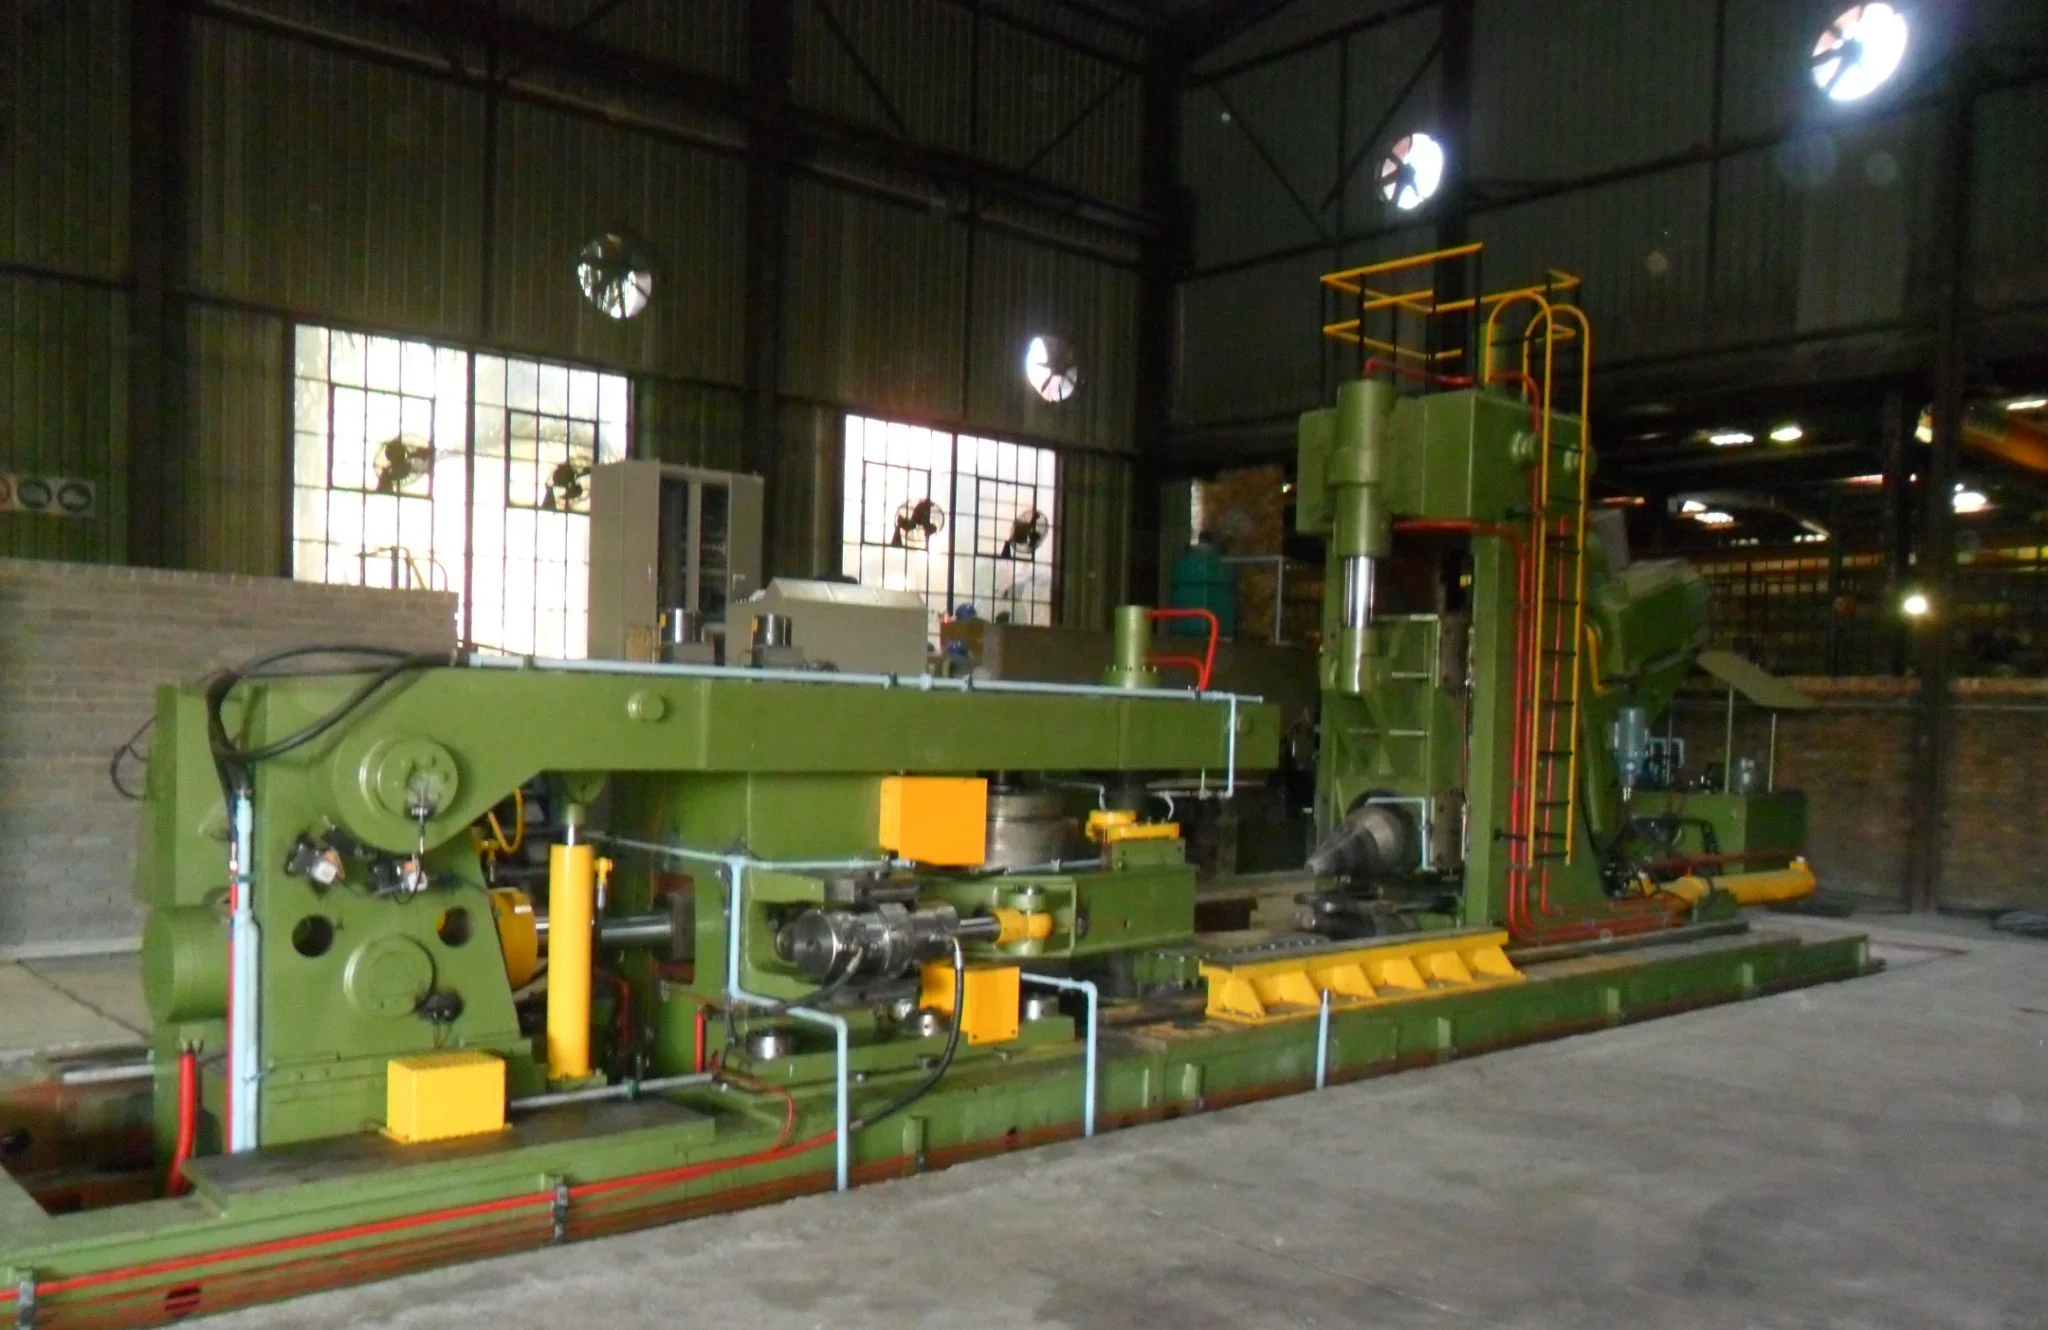
CNC Horizontal Ring Rolling Machine for Seamless Ring Forging
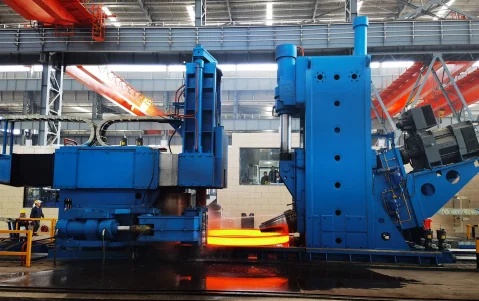
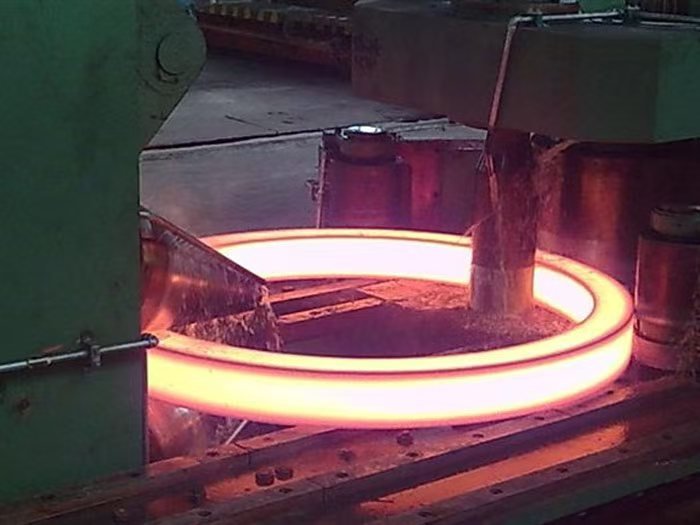
A CNC ring rolling machine forms a heated, pierced ring blank through controlled radial and axial rolling. Radial feed reduces wall thickness as the diameter grows; axial rolling controls ring height and the end faces.
Wiz Forging Machinery manufactures horizontal radial-axial ring rolling machines for ring forging applications. We review the hot blank and rolled ring dimensions, material grade, process route and output before specifying the machine and supporting equipment.
Our engineering and technical support cover machine configuration, equipment interfaces and installation planning within the agreed project scope.
What Is a CNC Ring Rolling Machine?
A CNC ring rolling machine gradually enlarges a heated ring blank by applying pressure through rolling tools. During the process, the ring diameter increases while the wall thickness and height are controlled. The radial rolling system forms the ring diameter and wall thickness, while the axial rolling system helps control ring height and end-face quality.
This type of machine is commonly used for producing seamless rolled rings with high material utilisation, consistent dimensions and improved production efficiency compared with cutting large rings from solid plate or welded fabrication.
Features
CNC Radial-Axial Rolling Control
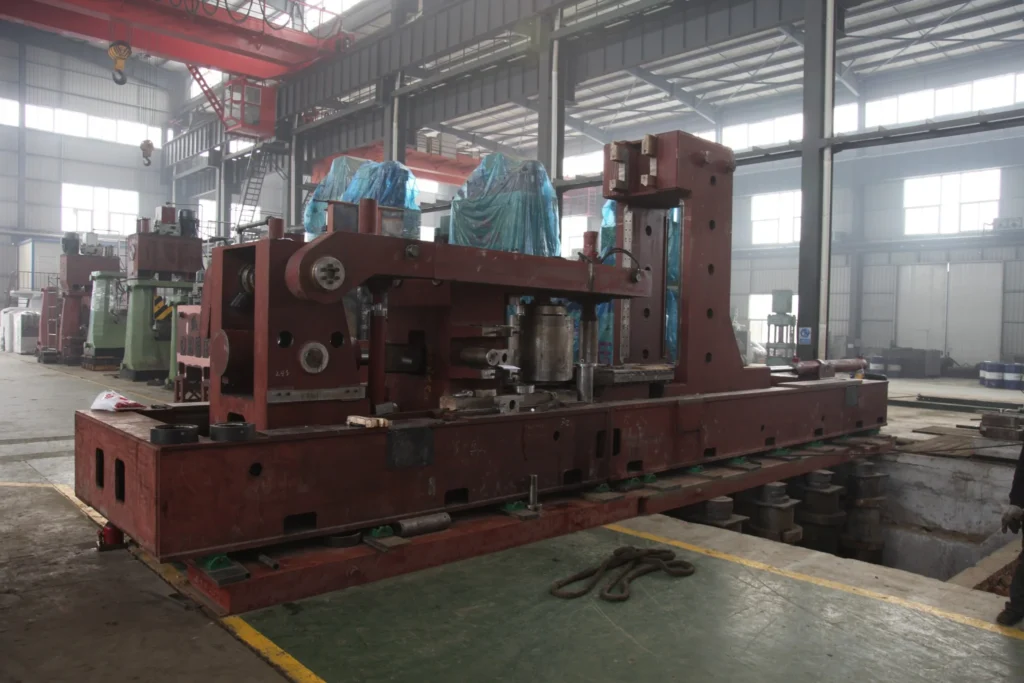
Heavy-Duty Horizontal Structure
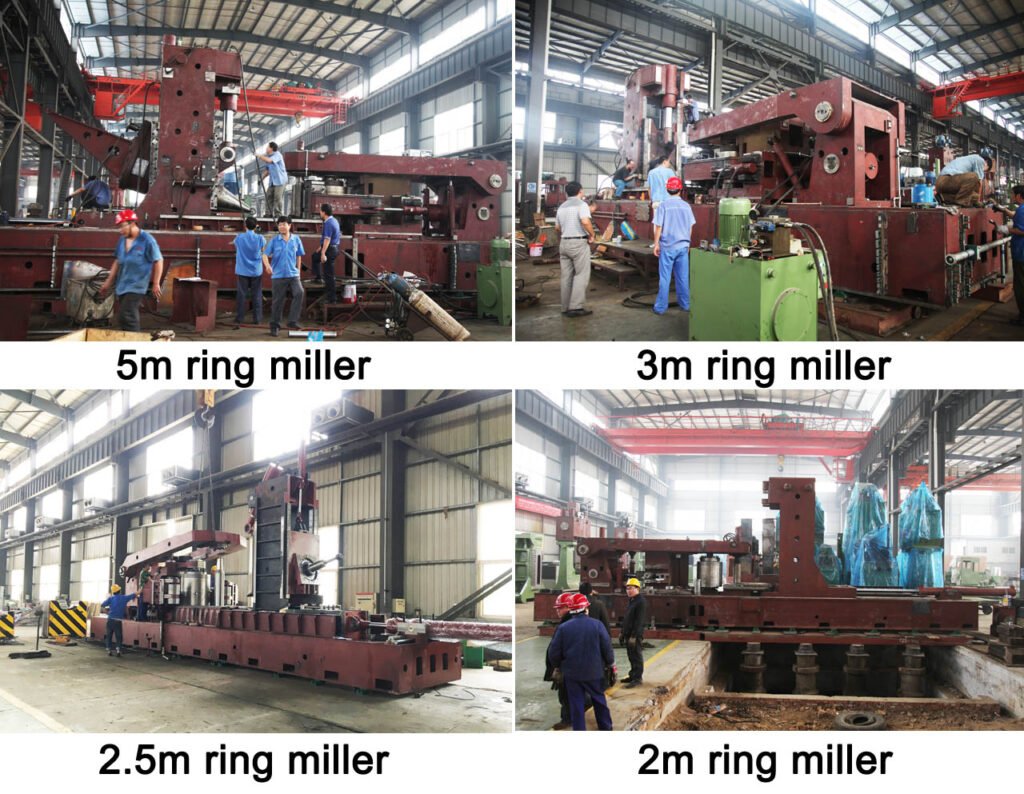
Wide Ring Size Capability
Strong Rolling Force
High Material Utilisation
Industrial Automation Options
How to Choose the Right CNC Ring Rolling Machine
Choosing the correct CNC horizontal ring rolling machine depends on more than the maximum ring diameter. Buyers should also consider blank size, ring height, finished wall thickness, material strength, rolling temperature, production tolerance, annual output and available workshop space.
For large flanges and wind power rings, rolling force and machine stability are critical. For bearing rings and gear blanks, dimensional control and repeatability are especially important. For alloy steel or stainless steel rings, the forming load, heating process and tooling design must be reviewed carefully.
Before recommending a model, Wiz Forging Machinery normally asks for the following information:
Ring outer diameter range
Ring inner diameter range
Ring height range
Finished wall thickness
Material grade
Ring drawing or sample product
Production quantity per shift or per month
Heating method
Automation requirement
Factory space and foundation conditions
Benefits
Better Ring Accuracy
Higher Production Efficiency
Lower Material Waste
Suitable for Large Forgings
Flexible Product Range
Strong Project Support
Typical Applications
Flange Ring Production
Used for producing forged flanges, welding neck flanges, pressure vessel flanges, pipe flanges and petrochemical connection rings.
Bearing and Gear Rings
Suitable for large bearing rings, gear blanks, slewing rings, transmission rings and mechanical drive components.
Wind Power and Heavy Industry Rings
Used for wind turbine flanges, tower connection rings, heavy machinery rings, marine components and large industrial ring forgings.
Aerospace and Energy Components
Suitable for high-performance ring forgings used in aerospace, nuclear, energy, oil and gas, and power generation industries.
Alloy and Stainless Steel Rings
Can be configured for carbon steel, alloy steel, stainless steel, aluminium alloy, copper alloy, titanium alloy and high-temperature alloy ring production.
Large Diameter Seamless Rings
Designed for large ring production where stable rolling, strong forming force and controlled dimensional accuracy are required.
Process Flow
Billet Heating
Piercing or Preforming
Radial and Axial Rolling
Size Monitoring
Final Ring Forming
Cooling and Finishing
Technical specifications
| Specification | Unit | WFM-1200 | WFM-2000 | WFM-3000 | WFM-5000 | WFM-6300 | WFM-6300H | WFM-7000 | WFM-10000 | WFM-12000 |
|---|---|---|---|---|---|---|---|---|---|---|
| Radial Rolling Force | kN | 1250 | 1600 | 2000 | 2500 | 4000 | 5000 | 6300 | 10000 | 16000 |
| Axial Rolling Force | kN | 800 | 1250 | 1600 | 2000 | 3150 | 4000 | 4500 | 8000 | 8000 |
| Radial Motor | kW | 315 | 2 × 200 | 2 × 280 | 2 × 400 | 2 × 500 | 2 × 630 | 2 × 630 / 800 | 2 × 1250 | 2 × 2000 |
| Axial Motor | kW | 250 | 2 × 200 | 2 × 280 | 2 × 400 | 2 × 500 | 2 × 630 | 2 × 630 | 2 × 1300 | 2 × 1300 |
| Rolling Ring Outer Diameter | mm | 400–1200 | 600–2000 | 700–3500 | 800–5000 | 900–6300 | 900–6300 | 900–7000 | 1250–10000 | 1500–12000 |
| Taper Roller Spacing | mm | 40–350 | 80–550 | 80–650 | 90–800 | 100–1000 | 100–1400 | 80–1350 | 110–1800 | 130–2000 |
| Maximum Rolling Height | mm | 300 | 420 | 500 | 600 | 850 | 1000 | 1200 | 1650 | 2200 |
| Finished Product Wall Thickness | mm | 120 | 200 | 250 | 300 | 420 | 500 | 540 | 800 | 800 |
| Machine Length | mm | 8500 | 13500 | 19000 | 21000 | 25000 | 27000 | 30000 | 40000 | 47000 |
| Machine Width | mm | 1930 | 2400 | 3400 | 4500 | 5800 | 6000 | 6500 | 8000 | 10000 |
| Height Above Ground | mm | 3850 | 5200 | 5800 | 6200 | 7200 | 8900 | 9200 | 10500 | 11500 |
| Application Scope |
Forging Process: Hot ring rolling, seamless ring forging, radial-axial rolling, ring diameter expansion, wall thickness control and height control Suitable Materials: Carbon steel, alloy steel, stainless steel, aluminium alloy, copper alloy, titanium alloy, high-temperature alloy and other forgeable metals Typical Products: Bearing rings, gear rings, flange rings, wind power flanges, welding neck flanges, hubs, thin-wall cylinders, petrochemical rings, aerospace rings and heavy machinery ring forgings |
|||||||||
| Note | The existing technical values are retained for reference and require confirmation for the project. The WFM-3000 outer-diameter entry is 700–3500 mm as listed. The WFM-7000 radial motor entry “2 × 630 / 800 kW” does not state the option basis. The finished wall-thickness figures do not specify minimum, maximum or nominal thickness. Taper roller spacing and maximum rolling height use different listed limits and must be clarified against the equipment drawing. Do not use these entries as guaranteed operating limits without an agreed technical specification. | |||||||||
For model selection, send your finished ring and forging drawings, material grade, hot blank dimensions and weight, rolling temperature, required tolerances and production output. Wiz Forging Machinery will review rolling capacity, tooling and the production route for your application.
Materials Suitable for CNC Ring Rolling
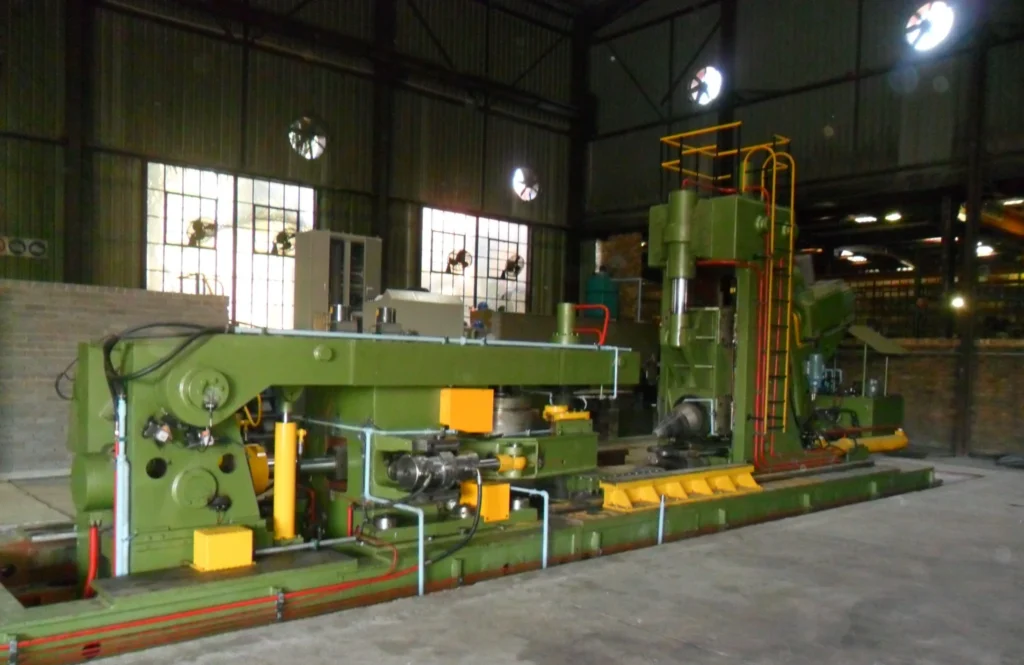
This machine range can be used for many forgeable materials depending on heating, tooling and rolling process design.
Carbon Steel and Alloy Steel
Commonly used for flanges, bearing rings, gear rings, heavy machinery parts and general industrial ring forgings.
Stainless Steel and Heat-Resistant Alloys
Suitable for pressure equipment, petrochemical components, energy equipment and corrosion-resistant ring products.
Non-Ferrous Alloys
Depending on configuration, machines can support aluminium alloy, copper alloy, titanium alloy and specialist metal ring production.
First forging machine questionnaire
Which machine do you need?
Take our quick questionnaire to discover which machine fits your needs. For an exact match and pricing, a detailed quote will be required.