Blog
How Does a CNC Hydraulic Closed Die Forging Hammer Work?
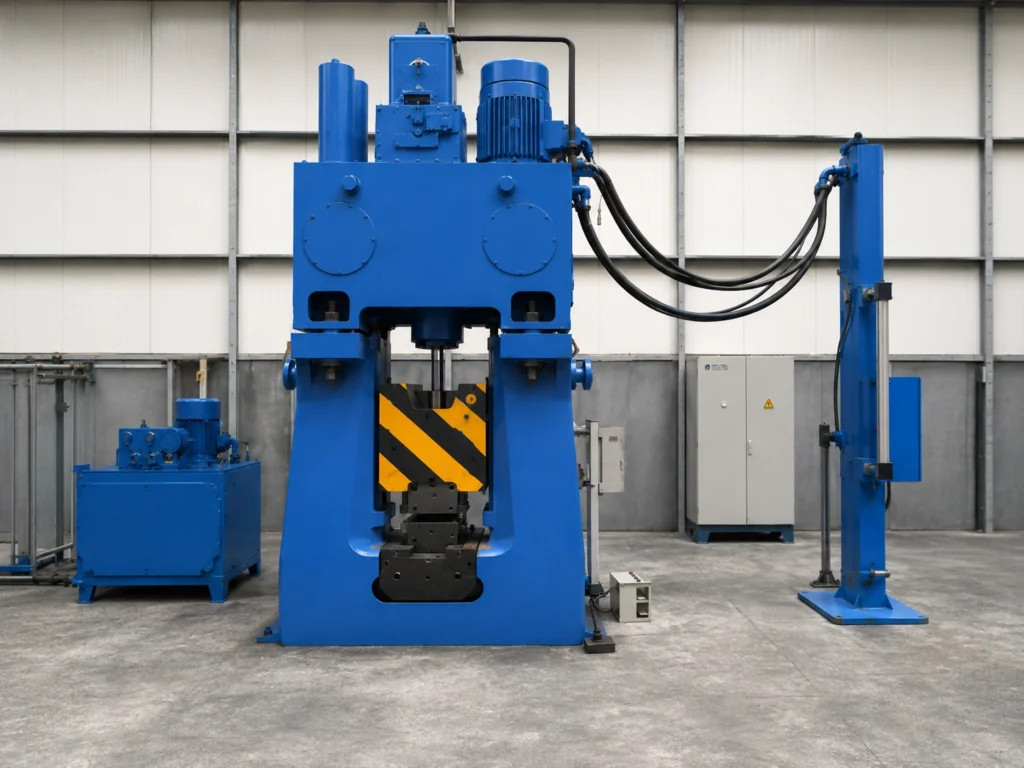
The working cycle begins with a heated billet positioned in the lower die. CNC instructions coordinate ram movement and selected blow energy while the hydraulic system drives the striking and return movements required for the planned forging sequence.
For available configurations and application support, visit our CNC Hydraulic Closed Die Forging Hammer machinery page.
This guide explains the technical questions buyers should review before selecting equipment, tooling or a production-line arrangement for this application.
Understanding how CNC hydraulic forging hammer works
The working cycle begins with a heated billet positioned in the lower die. CNC instructions coordinate ram movement and selected blow energy while the hydraulic system drives the striking and return movements required for the planned forging sequence.
The hammer and supporting equipment should be treated as one production system. Billet preparation, heating, transfer, die design, lubrication, trimming, cooling and inspection can all influence the final result.
Final recommendations should be based on reviewed project data and, where appropriate, trial forging or process calculations. Nominal model descriptions alone do not confirm suitability.
Key Technical Considerations
1. Billet preparation
Billet volume, cut quality and heating consistency affect material flow before the hammer delivers its first blow.
During technical confirmation, the relevant drawings, operating conditions and acceptance criteria should be recorded so the proposed arrangement can be checked against the actual application.
2. Loading and positioning
The billet must reach the die with the correct orientation and within the permitted temperature window. Manual, assisted or robotic loading can be considered.
During technical confirmation, the relevant drawings, operating conditions and acceptance criteria should be recorded so the proposed arrangement can be checked against the actual application.
3. CNC-controlled striking
The control system manages the selected sequence and energy settings. Recipes should be developed from trials and verified parts rather than copied between unrelated forgings.
During technical confirmation, the relevant drawings, operating conditions and acceptance criteria should be recorded so the proposed arrangement can be checked against the actual application.
4. Metal flow in the die cavity
Each blow moves heated material through the impressions. Preform design, flash land and lubrication influence whether the cavity fills evenly.
During technical confirmation, the relevant drawings, operating conditions and acceptance criteria should be recorded so the proposed arrangement can be checked against the actual application.
5. Return and part removal
The ram returns after the programmed action so the part can be transferred to trimming, cooling or the next forming operation.
During technical confirmation, the relevant drawings, operating conditions and acceptance criteria should be recorded so the proposed arrangement can be checked against the actual application.
Production-Line and Integration Considerations
Coordinating the Complete Forging Cell
A CNC hydraulic closed die forging hammer may operate as a standalone machine or within a coordinated line. Depending on the component, the line can include billet cutting, induction or other heating, temperature monitoring, feeders, robots, die lubrication, trimming, cooling and inspection equipment.
Interfaces should define ready signals, permitted movements, fault handling, emergency stops and safe maintenance conditions. Output should be assessed across the complete line because a restriction at heating, transfer, trimming or inspection can limit the practical production rate.
| Review area | What to confirm | Evidence required |
|---|---|---|
| Billet preparation | Billet volume, cut quality and heating consistency affect material flow before the hammer delivers its first blow. | Project drawings, process data and agreed acceptance criteria |
| Loading and positioning | The billet must reach the die with the correct orientation and within the permitted temperature window. | Project drawings, process data and agreed acceptance criteria |
| CNC-controlled striking | The control system manages the selected sequence and energy settings. | Project drawings, process data and agreed acceptance criteria |
| Metal flow in the die cavity | Each blow moves heated material through the impressions. | Project drawings, process data and agreed acceptance criteria |
| Return and part removal | The ram returns after the programmed action so the part can be transferred to trimming, cooling or the next forming operation. | Project drawings, process data and agreed acceptance criteria |
Suitable Applications
The subject covered in this guide may be relevant to suitable closed-die and impression-die hot-forging projects in automotive, hand-tool, hardware, agricultural machinery and general industrial component production.
Possible materials include carbon steel, alloy steel, stainless steel, aluminium alloys, brass and copper alloys, subject to grade-specific technical assessment. Application suitability depends on component geometry, material behaviour, billet, tooling and the planned production sequence.
How to Evaluate the Correct Configuration
Selection should consider the finished component and forging drawings, exact material grade, finished and billet weights, billet dimensions, forging temperature, projected area, die arrangement, number of stages and required output.
Buyers should also confirm the factory layout, lifting and maintenance access, utilities, foundation responsibilities, preferred loading method, safety requirements and downstream equipment. Existing equipment can only be included after its interfaces and capacity have been checked.
Materials and Component Suitability
Forgeable materials do not respond identically to heating and impact. The exact grade affects the permitted temperature range, flow behaviour, die material, lubrication, energy sequence and cooling or heat-treatment requirements.
Component weight on its own is not enough to select a hammer. Thin ribs, deep cavities, changes in section, projected area and the number of die impressions can materially change the process. Wiz Forging Machinery therefore reviews the component and process data before recommending a suitable WFM-style configuration.
Frequently Asked Questions
What should buyers understand about how CNC hydraulic forging hammer works?
The working cycle begins with a heated billet positioned in the lower die. CNC instructions coordinate ram movement and selected blow energy while the hydraulic system drives the striking and return movements required for the planned forging sequence.
How is the correct hammer or process configuration selected?
Selection should use the component and forging drawings, material grade, billet data, die sequence, required output, factory conditions and supporting-equipment scope.
Can the hammer be integrated with an automated forging line?
Yes, where the project supports automation. Heating, transfer, robot or feeder interfaces, die lubrication, trimming, cooling and safety controls must be designed as one coordinated system.
Which materials can be considered?
Carbon steel, alloy steel, stainless steel, aluminium alloys, brass, copper alloys and other forgeable metals may be considered, but the exact grade and forging route must be technically confirmed.
What information is needed before a quotation?
Provide the finished and forging drawings, material, weights, billet dimensions, heating method, die information, production target, factory voltage, layout and required commercial scope.
Information to Provide for a Quotation
For a useful technical and commercial review, please provide:
- Finished component and forging drawings
- Exact material grade and applicable standard
- Finished, forged and billet weights
- Billet dimensions and heating method
- Proposed die sequence and available tooling information
- Required hourly, shift and annual output
- Manual, assisted or robotic handling requirements
- Factory layout, voltage, frequency and utility conditions
- Required delivery, installation, training and documentation scope
Technical Review and Next Step
The working cycle begins with a heated billet positioned in the lower die. CNC instructions coordinate ram movement and selected blow energy while the hydraulic system drives the striking and return movements required for the planned forging sequence.
Wiz Forging Machinery can review the component, material, billet, tooling concept, output target and factory conditions before recommending a suitable CNC hydraulic closed die forging hammer and supporting line equipment.
Send the available project information for a technical review and quotation. Recommendations will be based on the confirmed application rather than unsupported standard-performance assumptions.