CNC Forging Manipulator Automation for Open Die Lines
Automation in an open die forging line depends on coordinating the manipulator with the press or hammer. Programmed feeding, rotation and positioning can support repeatable handling, but the control sequence must reflect the changing workpiece shape, equipment clearances and permitted machine movements.
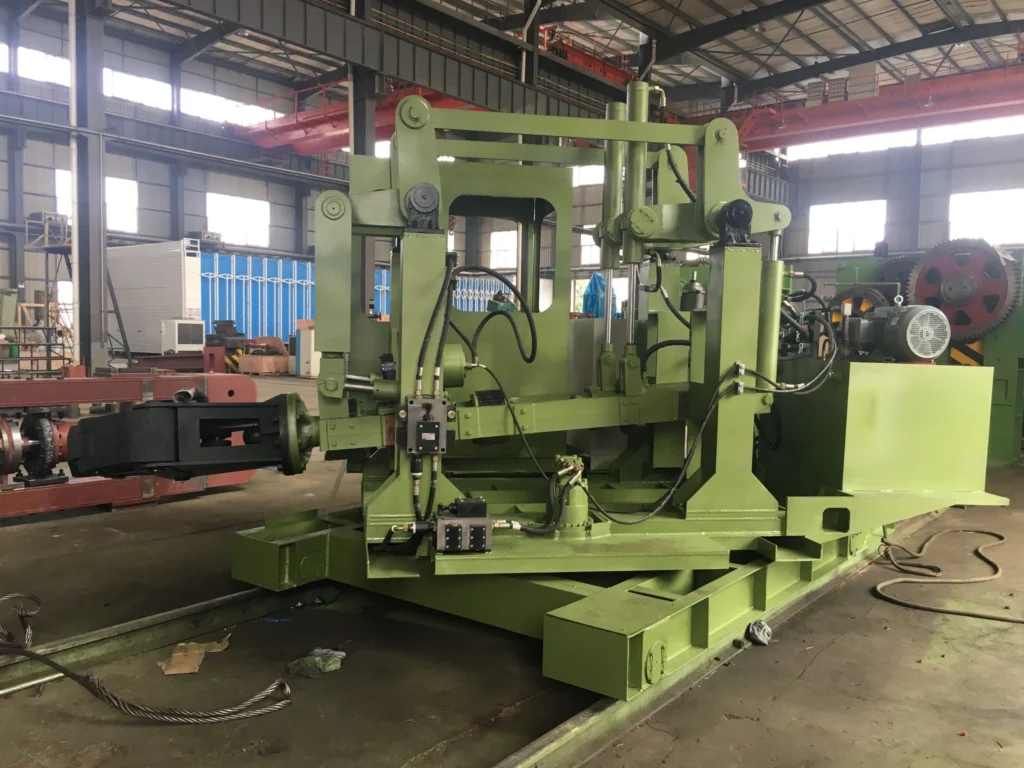
A CNC forging manipulator can clamp, lift, feed, rotate and reposition hot workpieces. This guide explains the process data, control interfaces and operating arrangements to confirm before specifying an automated handling system.
Understanding forging manipulator automation
Manipulator automation links handling movements to a defined forging sequence. A semi-automatic arrangement may execute selected steps under operator control, while a linked CNC system can coordinate programmed movements with the forging machine. The available functions depend on the agreed machine configuration and control interfaces.
Programme selection, position feedback, clamping confirmation and operator override must suit the workpiece range. A repeatable motion programme alone does not establish that the whole forging line can operate unattended.
Key Technical Considerations
1. Workpiece and Forging Process
Begin with the finished component and work backwards through the forging route. Confirm required automation level, position feedback, control interfaces, cycle sequence, operator override and safety philosophy. The heaviest or largest starting condition is important, but so are the intermediate shapes created as the billet is drawn, upset, rotated or reheated. A recommendation based on finished weight alone may not represent the most demanding handling condition.
2. Load, Clamping and Jaw Design
Rated load must be assessed together with workpiece geometry, centre of gravity and gripping position. Jaw opening and closing range, contact profile and clamping force should suit the actual hot dimensions. For round billets and shafts, a V-shaped arrangement may be suitable; special sections or pancake forgings can require a different jaw design.
3. Movement and Positioning Requirements
List every movement required during production, including travelling, feeding, lifting, lowering, lateral positioning, swinging and rotation. Define the order of these movements, the required strokes and speeds, and the conditions that permit each step. Check the programme against the workpiece envelope, die positions and clearances throughout the forging sequence.
4. Forging Machine Compatibility
The clamp centre height, forward reach and workpiece path must suit the working height and die area of the press or hammer. The practical integration requirement is that the manipulator must exchange the correct signals with the press, hammer, furnace and line safety system. Interface dimensions should be checked on an agreed layout drawing before manufacturing begins.
5. Controls, Automation and Safety
Manual, semi-automatic and CNC-linked control modes serve different production needs. The selected system should give the operator clear control of each permitted movement and include the required interlocks, emergency functions and status feedback. Automation should follow a verified forging sequence while retaining appropriate supervision and safe recovery procedures.
6. Layout, Installation and Service Access
Rail routes, foundation conditions, hydraulic power equipment, electrical cabinets and operator stations all require space. The final layout must also allow inspection of jaws, cylinders, hoses, wheels, rails and sensors. Planning only the production envelope and ignoring service access can make routine maintenance unnecessarily difficult.
Suitable Applications
CNC Forging Manipulator Automation for Open Die Lines may be considered for forging lines that require manual, semi-automatic or programmed workpiece feeding, rotation and repositioning. Suitability still depends on a technical review of the complete operating condition.
Open die and free forging operations
Billet, shaft, bar or ingot handling where applicable
Repeated feeding, rotation and repositioning
Integration with hydraulic presses or open die forging hammers
New production lines and compatible existing-machine upgrades
Materials can include carbon steel, alloy steel, stainless steel and other forgeable metals, subject to confirmation of temperature, surface condition, workpiece geometry and process requirements.
Production-Line Integration
The manipulator and forging machine need an agreed set of command, status and permissive signals. Confirm which controller requests a movement, which controller authorises it, and how position and clamping feedback are checked. Furnace and other handling interfaces should be included where the process requires them.
Define the response to a stopped cycle, loss of feedback, loss of power or a communication fault. Before commissioning, agree how an operator can inspect the workpiece, recover the sequence and return to automatic operation without creating conflicting commands.
Selecting the Correct Configuration
Selection should confirm required automation level, position feedback, control interfaces, cycle sequence, operator override and safety philosophy. Buyers should also define expected operating hours, production mix, future workpiece range and any need for manual, semi-automatic or linked operation.
A useful proposal explains the assumptions behind the recommended capacity, jaw range, movements, track arrangement and control system. If important information is missing, it is better to identify the gap than to present an unsupported final specification.
Information Buyers Should Provide for a Quotation
For a technical review and quotation, provide as much of the following information as possible:
Workpiece and forging drawings
Maximum and minimum hot workpiece weights
Billet, ingot or shaft dimensions at each important stage
Material grade and forging temperature
Press or hammer type, capacity and working height
Required manipulator movements and control mode
Factory layout, rail route and available utilities
Target production rate and operating schedule
Photographs and drawings of existing equipment can help identify interface constraints, but final dimensions should be confirmed from controlled technical documents.
Frequently Asked Questions
What is forging manipulator automation used for?
It coordinates programmed feeding, rotation and positioning with the forging sequence. The functions available depend on the agreed controller, feedback devices and interfaces with the press or hammer. Operator supervision and recovery arrangements must be specified separately.
How is the correct manipulator capacity selected?
Capacity is reviewed from the maximum handling condition, workpiece geometry, centre of gravity, gripping position, required movements and an appropriate engineering margin. Finished component weight alone is insufficient.
Can it work with an existing forging press or hammer?
Often yes, provided the working height, die area, clearances, travel route, controls and safety interfaces are compatible. An existing-machine survey is normally required.
Can the clamping jaws be customised?
Jaw design can be reviewed for round billets, shafts, ingots or special workpiece shapes. The hot dimensions, gripping surface and required rotation must be confirmed before the jaw arrangement is finalised.
What should be checked before placing an order?
Confirm the approved specification, layout, workpiece range, interfaces, utilities, foundation responsibilities, control philosophy, inspection requirements, commissioning scope and technical documentation.
Final Technical Review
Before specifying an automated forging manipulator, review the workpiece range, forging sequence, equipment interfaces, layout and control responsibilities together. Confirm how the system handles intermediate shapes, interrupted cycles and changes between production programmes.
Wiz Forging Machinery can review your drawings and production requirements to help define a suitable CNC forging manipulator configuration. Final functions, performance and specifications should be recorded in the approved technical agreement.
Discuss Your Forging Line Automation Requirements
Send your workpiece drawings, material, hot dimensions, weight range, forging-machine details and factory layout to Wiz Forging Machinery for a technical review.
Use the separate machinery button to view our CNC Forging Manipulator range, or request a quotation for your project.